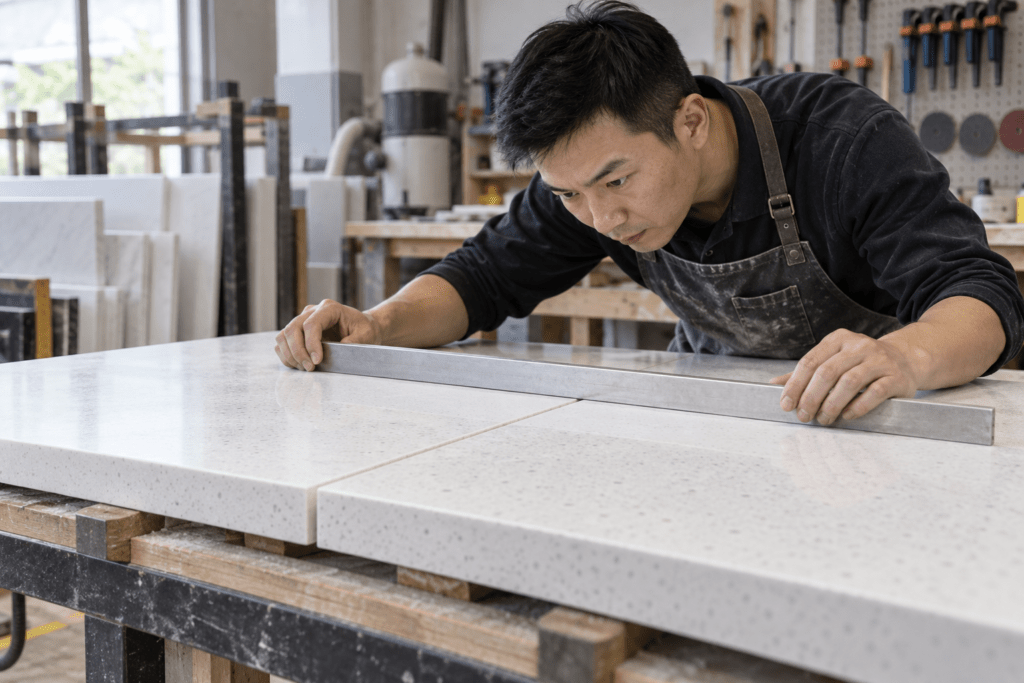
When a solid surface sheet arrives with a straight-looking factory edge, it can be tempting to use that edge directly for a joint. Trimming takes time and uses some material, but an edge that looks straight from a distance is not necessarily ready for bonding.
Before deciding whether to use it, consider what the edge has experienced—and what a successful joint requires.
Why a factory edge may not be ready for a seam
During production, packing, shipping and unloading, sheet edges can be exposed to minor chips or impact damage, dust, contamination, uneven saw marks, film residue or small variations that prevent consistent contact. A clean-looking edge is not proof that it is sufficiently flat, square or suitable for the adhesive system.
HIMACS advises fabricators to trim factory ends and edges before fabrication because those edges may have been damaged or contaminated, and the original cut may not provide an optimal surface for joining. This product-specific guidance illustrates why the edge needs to be assessed rather than assumed ready.
What can happen if edges are poorly prepared?
Possible outcomes include a wider or more visible joint line, inconsistent adhesive thickness, local gaps, a defect remaining inside the joint, and additional sanding or rework. A visible line is not automatically evidence of a weak joint, and a neat-looking joint does not by itself prove the bond is sound. Quality depends on preparation, adhesive, curing, support and material selection.
Step 1: Inspect the sheet before cutting
Check and record the colour and product reference, thickness and dimensions, batch or sheet number, and any visible damage. If you suspect a manufacturing or shipping issue, take photographs and contact the supplier before cutting. Once the material has been altered, it may become harder to assess its original condition or agree on a remedy.
For multi-sheet projects, record batch numbers and review the manufacturer’s colour-matching recommendations. HIMACS, for example, recommends checking sheet numbers and using sheets from the same lot for colour consistency where applicable.
Step 2: Allow for trimming in the cutting plan
Edge preparation should be part of the original material calculation. Allow for trimming factory edges where required, saw or router kerf, final joint preparation, necessary tolerances and any unsuitable or damaged edge area. This prevents discovering too late that parts fit on paper but not after the edges have been prepared.
For example, when two pieces meet at a visible seam, include the material removed when both mating edges are finished—not only the nominal finished dimensions. The exact allowance depends on the equipment, sheet condition and fabrication method; agree it with the workshop.
Step 3: Prepare the mating edges as a pair
Follow the sheet and adhesive manufacturers’ instructions for the approved cutting and routing method. The aim is to produce two clean, compatible edges that fit consistently along the joint.
Before applying adhesive, dry-fit the pieces and check the full length for rocking, gaps, chips and uneven contact. Confirm face and pattern orientation and agree whether any colour or pattern mismatch is acceptable. Do not use excess adhesive as a substitute for accurate edge preparation.
For patterned or veined colours, a sound joint can still be visually noticeable if the pattern does not align. Review the expected appearance with the customer before bonding.
Step 4: Control cleaning and bonding conditions
Use the cleaning method and adhesive specified or approved for the material. Verify compatibility with the exact sheet grade, shelf life and storage conditions, mixing and dispensing, working and curing conditions, clamping pressure and required joint support or reinforcement.
Do not select a solvent simply because it worked on a different brand. Confirm it against the current instructions for the material and adhesive in use.
Step 5: Keep a useful workshop record
For projects with multiple joints, retain the drawing and revision, sheet references and batch numbers, adhesive identification and batch where available, bonding date, unusual conditions or deviations, and photographs before closure and after finishing. These details help the supplier and fabricator investigate a later concern.
Frequently asked questions
Must every factory edge always be trimmed?
Follow the current instructions for the specific sheet and application. Some manufacturers explicitly recommend trimming factory edges before fabrication. If guidance is unclear, ask the supplier what preparation is required for bonding.
Can sanding alone make an edge ready for bonding?
That depends on the approved fabrication method. The edge must meet requirements for fit, geometry and surface condition; an edge that feels smooth is not necessarily properly prepared.
Can a damaged edge be used if the damage will be hidden?
Do not assume the adhesive will solve the problem. Assess the damage and follow the supplier’s instructions. If in doubt, remove the damaged area and obtain guidance before proceeding.
Final thought
Factory edges are useful reference points, but a joint needs a deliberately prepared bonding surface. Inspecting, planning and dry-fitting can prevent expensive rework after installation.
Related reading: how to check sheet flatness before cutting and how to create solid surface joints.